In the pharmaceutical and API manufacturing sectors, selecting a mixer is never a straightforward decision. The sheer number of variables involved—regulatory compliance, process traceability, validated cleaning procedures, and product integrity—makes every capital equipment selection a critical strategic choice.
Too often, buyers focus exclusively on the machine itself. However, the complete solution—comprising technical support, engineering expertise, and lifecycle service—is the true deciding factor when selecting a long-term partner.
This is precisely why MC² was founded.
Backed by over 30 years of powder handling expertise, MC² acts as a strategic technical partner rather than just an equipment manufacturer. We support pharmaceutical companies through every stage of the plant lifecycle, delivering bespoke engineering, seamless commissioning, routine maintenance, original spare parts, and 24/7 emergency support.
Bespoke customisation: because no two processes are alike
Every pharmaceutical facility operates under unique constraints—whether handling materials with varying bulk densities, managing strict containment levels, injecting liquids, or dosing micro-ingredients.
To overcome these challenges, MC² engineers dedicated, application-specific units. We collaborate closely with clients to select the optimal mixing drum geometry and materials of construction. Furthermore, we integrate high-performance sealing systems to guarantee absolute safety, and tailor charging and discharging ports around your exact operational workflows.
This tailored approach is not an optional extra or a premium service; it is simply our standard way of working.
Sanitary design: minimising downtime, maximising productivity
In the pharmaceutical industry, product changeovers and validated cleaning procedures are not ancillary activities: they are integral to the production process.
Engineered specifically for the pharmaceutical sector, MC² mixers feature effortless maintenance access, zero dead zones, and premium surface finishes that ensure absolute compatibility with rigorous sanitisation protocols.
This drastically reduces cleaning downtime and maximises production throughput, while completely eliminating the risk of cross-contamination.
MetaMix: the laboratory revolution
The journey of bringing a formulation from development to full industrial scale begins in the laboratory—the ultimate proving ground.
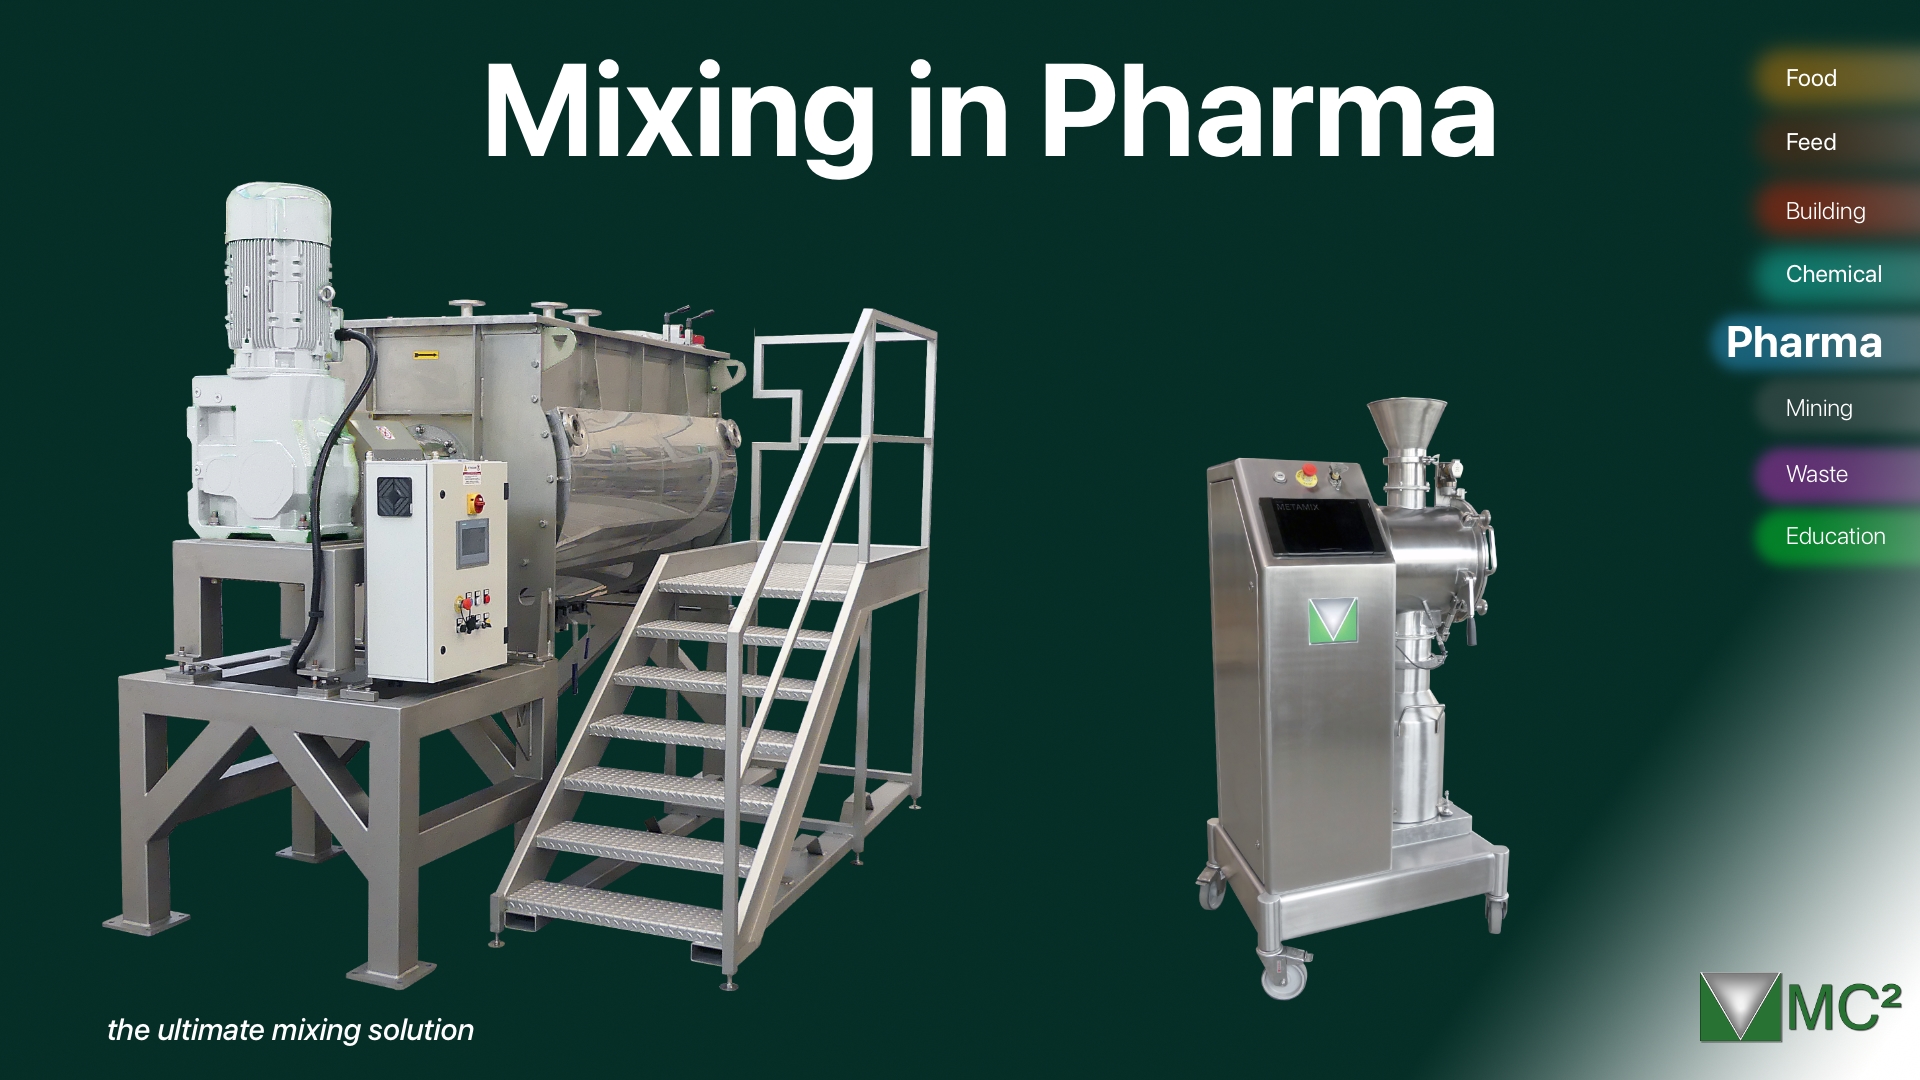
This is exactly why MC² developed MetaMix: a laboratory mixer engineered to meet the pharmaceutical industry's most stringent standards for precision, hygiene, and process control.
MetaMix is more than just a generic laboratory mixer—it is a comprehensive process system featuring:
- A mirror-polished 316L stainless steel mixing drum, guaranteeing the highest level of hygiene and effortless sanitisation.
- Interchangeable mixing technologies: swap between ploughs, paddle blades, and ribbon spirals to test different mixing technologies on the same formulation using a single unit, reducing development times and laboratory footprint.
- Latest-generation tablet control, features manual, automatic and remote operation via an intuitive interface with virtually no learning curve.
- Full FDA 21 CFR Part 11 compliance, with IQ/OQ validation protocols available upon request. Data integrity, traceability, and process validation are embedded into the unit’s DNA, not added as an afterthought.
MetaMix is available in both desktop and mobile versions (on castors) to adapt to your laboratory layout, not the other way round.
In short, the data generated by MetaMix transfers seamlessly to full-scale production equipment. This mitigates scale-up risks and accelerates time-to-market for new products
"You are not just buying a mixer; you are investing in a partner specialised in every stage of the mixing process, from formulation development to mass production."
The bottom line
The MC² ecosystem delivers tangible value by reducing operational risks, increasing process predictability, and lowering the total cost of ownership over the equipment’s lifespan.
When evaluating your options, look beyond the initial purchase price. Consider the cost of unforeseen downtime, a poorly validated cleaning process, or a failed scale-up that forces your team back to the drawing board.
When the efficacy of a medicine or the purity of an active ingredient is on the line, choosing the right partner is non-negotiable.